China’s sugar processing sector serves beverage, confectionery, dairy, bakery, and pharmaceutical applications. Recent USDA Sugar: World Markets and Trade reports place global centrifugal sugar production above 180 million metric tons annually. This scale increases demand for stable, hygienic, and efficient sugar syrup filtration systems.
Filtration quality affects syrup clarity, color, microbial control, and downstream equipment protection. China’s leading manufacturers commonly offer bag filters, cartridge filters, self-cleaning strainers, and stainless-steel pipeline systems. Buyers should examine flow rate, Brix level, syrup temperature, viscosity, filtration accuracy, and clean-in-place compatibility. These details matter. A filter rated at 100 microns may perform differently under concentrated syrup conditions.
FAO Food Outlook reports continue to monitor sugar production, trade, and food-processing pressures worldwide. Meanwhile, Codex food hygiene principles and ISO 22000 provide useful references for sanitary design, hazard control, and traceability. These sources support a practical evaluation framework for China’s top sugar syrup filtration manufacturers. Factory experience, material certificates, validation records, and after-sales response deserve equal attention. A polished brochure is not enough.
Some supplier rankings remain subjective. Public information can be incomplete. Therefore, this guide compares manufacturers through technical capability, documented project experience, stainless-steel quality, customization, testing procedures, and service reliability. The strongest supplier may not offer the lowest quotation. It should deliver clean syrup, repeatable performance, and safer production across changing operating conditions.
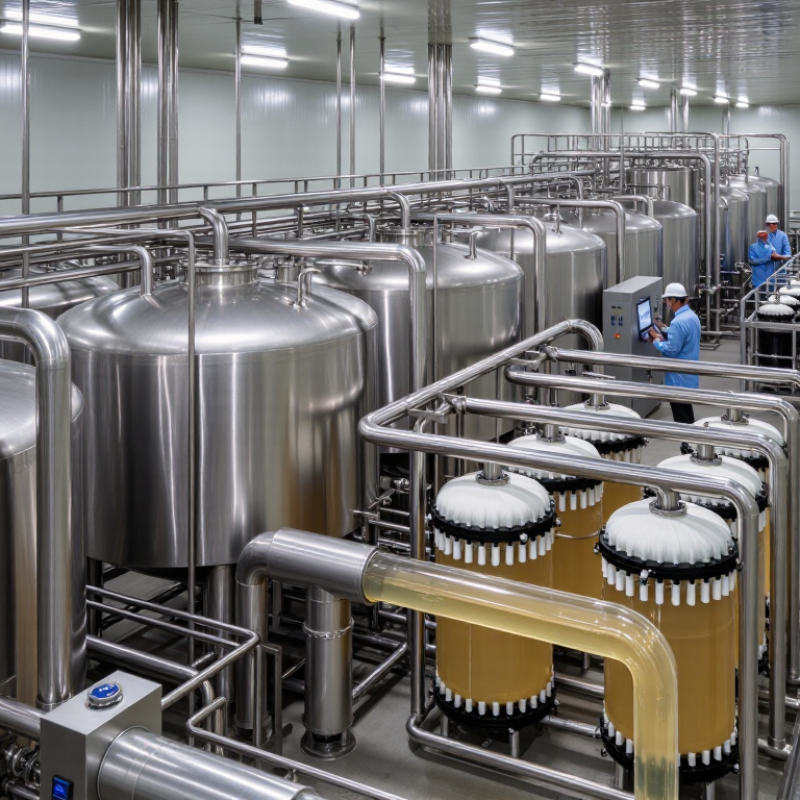
Sugar syrup filtration removes suspended solids, carbon fines, scale, and processing debris before filling or further blending. Clean syrup improves appearance, protects pumps, and reduces deposits in heat exchangers. It also supports consistent taste and color.
The principle is simple: syrup passes through a porous medium while unwanted particles remain on its surface or inside its depth structure. Filter selection depends on viscosity, temperature, flow rate, sugar concentration, and required clarity. Coarse filtration may protect equipment, while finer filtration improves visual quality. However, filtration cannot replace proper sanitation or microbial control. A filter is not a cure-all.
Reliable manufacturers in China should provide food-contact materials, hygienic connections, pressure-rated housings, and documented filtration performance. Their equipment should support clean-in-place procedures and allow easy inspection. Production teams should verify pore size, pressure loss, flow capacity, and seal compatibility through practical trials. Applicable food safety, electrical, pressure, and workplace standards must also be reviewed for the installation location.
Tips: Keep syrup temperature stable during testing. Record inlet and outlet pressure. Replace media before blockage affects flow. Ask for material certificates, test records, and cleaning guidance. Do not trust “absolute filtration” claims without test conditions. In real plants, operators sometimes choose finer media too quickly. This can increase costs and shorten service life. A balanced, documented approach is safer.
China’s sugar syrup filtration manufacturers increasingly combine mechanical separation with membrane polishing. Their systems often use stainless steel housings, sanitary valves, and food-grade seals. These materials support clean processing and reduce contamination risks.
Pre-filtration commonly uses bag or cartridge filters to remove crystals, fibers, and suspended solids. Finer membrane stages can reduce haze and improve visual clarity. Some facilities also use activated carbon for color adjustment, but dosage requires careful testing. Excessive treatment may reduce desirable flavor compounds. Automated pressure sensors help operators detect blockage before flow drops sharply. CIP systems use controlled rinsing, alkaline cleaning, and final sanitation cycles. However, cleaning results still depend on syrup temperature and residue age. This part is often underestimated.
Tips: Confirm the syrup’s viscosity, temperature, and target clarity before selecting equipment. Ask for test data using your actual syrup. Check filter compatibility, flow rate, replacement access, and CIP validation records. A lower micron rating is not always better. It may increase pressure loss and operating costs. Experienced manufacturers should explain these trade-offs clearly, rather than promise perfect filtration without process evidence.
The chart presents representative nominal separation thresholds commonly used in sugar syrup processing. Coarse screens remove larger solids first, followed by depth filters, cartridge filters, and membrane systems for progressively finer clarification. Actual specifications vary according to syrup concentration, temperature, viscosity, and required product quality.
Choosing among China’s top sugar syrup filtration manufacturers requires more than comparing prices. Start with process data: syrup viscosity, temperature, flow rate, sugar concentration, and target clarity. Ask whether the supplier can recommend cartridge, bag, plate, or membrane filtration with evidence. Request drawings showing sanitary welds, drainability, gasket materials, housing finish, and pressure limits. Equipment touching syrup should have traceable material records, not vague claims. Small details matter.
Trial results, transparent documents, and careful questions provide stronger evidence, although every evaluation can miss something.
Sugar syrup filtration supports clarity, consistency, and safer handling across food and beverage production. USDA Foreign Agricultural Service data projects global sugar production at about 189 million metric tons in 2024/25. That scale increases pressure on processors to control fibers, crystals, carbon particles, and equipment debris before blending.
In beverage plants, filtration protects dosing pumps, heat exchangers, filling valves, and spray nozzles. Bag or cartridge filters commonly remove visible particles after syrup dissolving. Finer membrane systems can support polishing before soft drinks, flavored water, sauces, and dairy beverages enter final processing.
A practical line may use staged filtration, such as 25 microns, then 5 microns. Clean-in-place design matters.
Food manufacturers also filter syrups used in bakery fillings, confectionery coatings, canned fruit, and nutritional products. The FAO Food Outlook 2024 highlights continuing pressure on food supply chains, making yield and process reliability important.
Filtration can reduce batch losses, but it cannot correct poor sanitation or unstable raw materials. That mistake still appears in real factories.
Chinese filtration manufacturers often provide stainless-steel housings, sanitary seals, pressure monitoring, and customized flow rates.
Validation should include turbidity, differential pressure, microbial results, and filter integrity testing. Performance claims without plant trials deserve caution.
Quality, Customization, and Export Support in China’s Filtration Industry
Reliable sugar syrup filtration starts with practical factory experience. Manufacturers should understand high viscosity, sticky residues, and temperature changes during production. A well-designed system may use sanitary stainless steel, polished welds, secure seals, and easy-to-clean filter housings. These details affect hygiene and daily maintenance.
Quality must be measurable. Buyers can request material certificates, pressure-test records, filter ratings, and traceable inspection reports. Sampling is also valuable. A syrup sample can reveal flow resistance, filter life, and cleaning requirements before full production. Small tests matter.
Customization is often necessary. Flow rates, syrup concentration, inlet temperature, and available floor space vary between facilities. Chinese manufacturers can adapt housing sizes, filtration stages, pump connections, control panels, and skid layouts. Some projects need manual operation. Others require automated pressure monitoring and alarm functions.
Export support should extend beyond the equipment itself. Clear drawings, installation instructions, spare-parts lists, strong export packaging, and responsive technical communication reduce installation risks. Manufacturers experienced with international shipments can also prepare accurate documentation and provide remote commissioning guidance.
Not every proposal is equally practical. A lower price may hide weak seals or difficult cleaning access. I would review these points carefully, even when delivery schedules look attractive. The best supplier is not always the fastest. It is the one that documents performance honestly and adjusts the design when operating conditions change.
Copyright © 2021 Payless Pet Products - All Rights Reserved.