What Is a Threaded Shaft End?
When a shaft must connect with a nut, coupling, bearing, or retaining component, its end often needs a precise threaded section. A Threaded Shaft End is the prepared portion where helical threads allow another part to attach securely. It may use external threads, internal threads, or a threaded stud fitted into the shaft. This design transfers rotation, axial force, or clamping pressure through a compact connection.
The thread is only one part of the engineering decision. Diameter, pitch, thread form, thread length, shoulder position, and material strength all affect performance. A fine thread can provide accurate adjustment, while a coarse thread may resist damage during repeated assembly. Small details matter. A shaft that fits visually may still have the wrong pitch or insufficient engagement.
In practical work, technicians measure the major diameter with calipers and verify the pitch with a thread gauge. They also inspect the first thread, runout, surface finish, and shoulder condition. Experienced machinists know that burrs near the shoulder can prevent a nut from seating correctly. That assumption can be wrong.
Manufacturers may define dimensions through recognized engineering standards, but terminology can vary between industries and suppliers. Therefore, drawings and technical data should control the final specification. During installation, correct torque, suitable lubrication, and thread protection reduce galling and premature wear. A damaged thread should not be forced into service. Careful inspection remains essential, especially where vibration, heat, or heavy loads are present. Understanding these details makes the threaded shaft end easier to identify, specify, and maintain reliably.
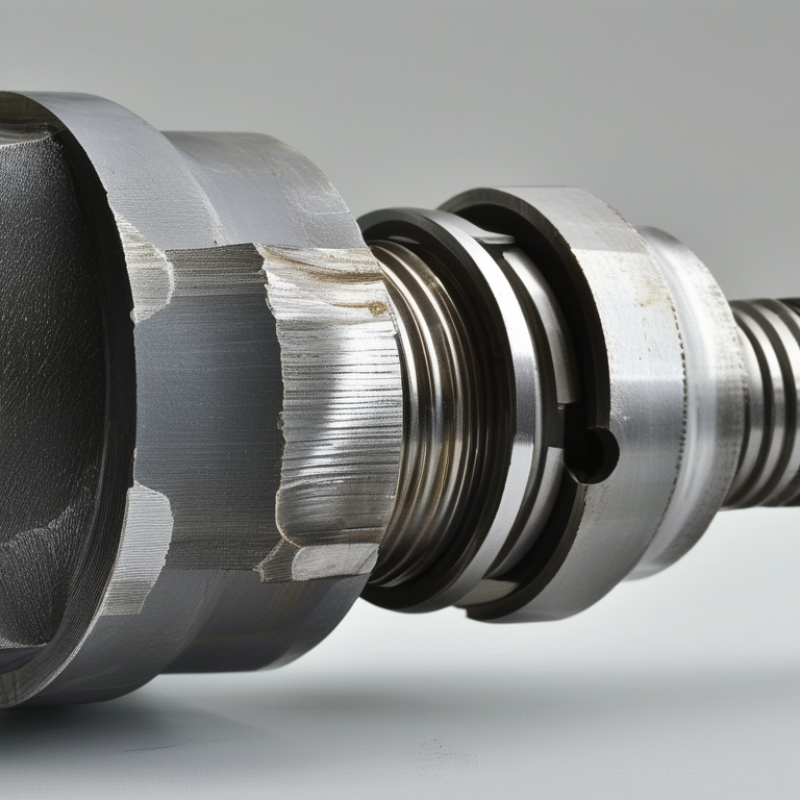
Definition and Function of a Threaded Shaft End in Mechanical Assemblies
What Is a Threaded Shaft End?
Definition and Function of a Threaded Shaft End in Mechanical Assemblies
A threaded shaft end is the portion of a cylindrical shaft machined with helical grooves. These grooves accept a nut, threaded hub, or retaining component. In mechanical assemblies, the threaded section creates a controlled axial connection. The shaft carries torque, while the threads usually carry clamping force. That distinction matters. A thread can look strong yet fail under unexpected bending.
During assembly inspections, I check thread pitch, major diameter, crest condition, and shoulder contact. A clean shoulder is essential. It gives the mating part a firm seating surface. The nut should tighten against the shoulder, not damaged threads or a burr. Engineers choose coarse or fine threads according to load, vibration, adjustment, and available space. Fine threads allow precise adjustment, but dirt can affect them more easily. Lubrication also changes tightening behavior, so torque values must match the specified condition.
A threaded shaft end may secure bearings, pulleys, couplings, or linkages. It can also provide controlled preload for bearings. A common mistake is assuming a tight nut proves a reliable assembly. It does not. The fit may look right, yet behave wrong. An undersized shoulder, worn thread, or poor alignment can allow loosening. Measuring with a thread gauge and checking shaft runout can reveal problems early. Even accurate drawings deserve practical review, because real loads are rarely as neat as calculations.
| Dimension or Feature | Definition or Typical Data | Mechanical Function | Design and Assembly Notes |
|---|---|---|---|
| Basic definition | A threaded shaft end is the portion of a cylindrical shaft that contains helical threads, normally on the outside diameter. | Allows components such as nuts, hubs, bearings, collars, or couplings to be secured to the shaft. | The threaded section should be concentric with the shaft axis and manufactured with a suitable surface finish. |
| Common thread form | Metric ISO 60-degree V-thread, commonly specified as M6 × 1.0, M8 × 1.25, M10 × 1.5, M12 × 1.75, M16 × 2.0, or M20 × 2.5. | Provides standardized compatibility between the shaft end and mating internally threaded parts. | The designation gives the nominal thread diameter in millimetres followed by the pitch in millimetres. |
| Nominal diameter | Typical external-thread sizes range from approximately 6 mm to 20 mm in light- and medium-duty assemblies. | Influences the tensile, shear, and torsional capacity of the threaded connection. | The effective load capacity is lower than that of a plain shaft with the same outside diameter because material is removed to form the thread. |
| Thread pitch | Typical coarse metric pitches include 1.0 mm for M6, 1.25 mm for M8, 1.5 mm for M10, 1.75 mm for M12, 2.0 mm for M16, and 2.5 mm for M20. | Determines axial movement per revolution and affects tightening speed, self-locking behavior, and thread strength. | Fine-pitch threads may provide greater adjustment precision and improved resistance to loosening, but they require closer control of contamination and damage. |
| Threaded length | Common threaded lengths are approximately 1 to 2 times the nominal diameter, depending on the load and application. | Provides sufficient engagement for transferring axial and tightening loads. | Actual engagement length must be calculated from load, material strength, thread class, and the strength of the mating nut or component. |
| Thread engagement | For steel-to-steel connections, an engagement length near one nominal diameter is often used as an initial design reference; softer materials generally require more. | Controls resistance to thread stripping and pull-out. | This is a preliminary guideline, not a universal rule. Engineering calculations are required for highly loaded or safety-critical joints. |
| Thread tolerance class | Metric external threads are commonly specified with classes such as 6g, while internal threads may use a class such as 6H. | Controls the fit, clearance, interchangeability, and assembly torque of the mating parts. | The selected tolerance should allow assembly without excessive play while preventing binding under normal operating conditions. |
| Thread runout and relief | A relief groove or runout area may be provided between the threaded portion and the unthreaded shaft. | Allows the cutting tool to exit cleanly and enables the mating component to seat against a shoulder. | Adequate relief reduces incomplete threads and helps prevent stress concentration at the thread termination. |
| Shoulder and seating surface | Many threaded shaft ends include a shoulder, spacer seat, or machined locating surface adjacent to the threads. | Positions the mounted component axially and transfers clamping or reaction forces. | The shoulder face should be square to the shaft axis when accurate bearing or hub alignment is required. |
| Typical shaft-end components | Nuts, locknuts, washers, spacers, retaining collars, bearings, hubs, sprockets, pulleys, and couplings. | Creates a removable connection without welding, permanent bonding, or complex external clamps. | Use a washer or dedicated seating face when the mating component could be damaged by the nut or tightening force. |
| Primary loads | Axial tension, axial compression, preload, torsion, bending, and localized bearing loads may act on the threaded end. | Allows the joint to retain components and resist movement during operation. | Threads are especially sensitive to combined loading and bending near the first engaged thread; avoid using a threaded section as a high-bending region when possible. |
| Locking methods | Common methods include a prevailing-torque nut, locknut, castellated nut with a retaining pin, tab washer, thread-locking compound, or safety wire. | Reduces the risk of loosening caused by vibration, cyclic loading, or changes in temperature. | The locking method must be compatible with the service temperature, lubrication, maintenance requirements, and required disassembly frequency. |
| Common materials | Carbon steel, alloy steel, stainless steel, and aluminium alloys are frequently used for shafts and threaded ends. | Material selection determines strength, corrosion resistance, weight, wear resistance, and machinability. | When using dissimilar metals, consider galvanic corrosion, thread galling, and the need for suitable lubrication or surface treatment. |
| Surface protection | Possible treatments include oiling, zinc-based coatings, black oxide, passivation, or other application-specific finishes. | Protects the threaded end from corrosion and preserves the fit between mating threads. | Coating thickness can alter thread fit and tightening behavior, so coated threads should be specified and inspected accordingly. |
| Manufacturing methods | Threads may be produced by single-point turning, die cutting, thread milling, or thread rolling. | Creates the helical profile needed for the mating connection. | Thread rolling can improve fatigue performance by displacing material and producing beneficial surface properties, while cutting methods are flexible for low-volume or large-diameter work. |
| Inspection requirements | Typical checks include nominal diameter, pitch, thread length, runout, visual damage, and fit with a calibrated mating gauge. | Confirms interchangeability and helps prevent assembly failure. | For critical assemblies, inspect thread form, concentricity, surface defects, hardness, and dimensional compliance with the specified drawing or standard. |
| Applicable thread standards | Metric threads are commonly defined using ISO 261 and ISO 965; unified inch threads may be specified using ASME B1.1. | Provides consistent thread geometry, dimensions, tolerances, and interchangeability. | The drawing should state the thread standard, nominal size, pitch or threads per inch, tolerance class, handedness, and threaded length. |
| Right-hand and left-hand threads | Right-hand threads are standard; left-hand threads are used where rotation could loosen a conventional right-hand thread. | Helps maintain the connection under a known direction of rotation. | Left-hand threads must be clearly marked because they are not interchangeable with standard right-hand mating parts. |
| Key advantage | Provides a compact, strong, adjustable, and removable method of retaining parts on a shaft. | Supports maintenance, replacement, preload adjustment, and controlled axial positioning. | Correct thread specification, adequate engagement, proper tightening, and suitable locking are essential for reliable service. |